Try Safe in one click and discover how we improve your occupational risk prevention

No-obligation trial

FOOD INDUSTRY

Occupational Health & Safety in the food industry

Safety at every stage of production.

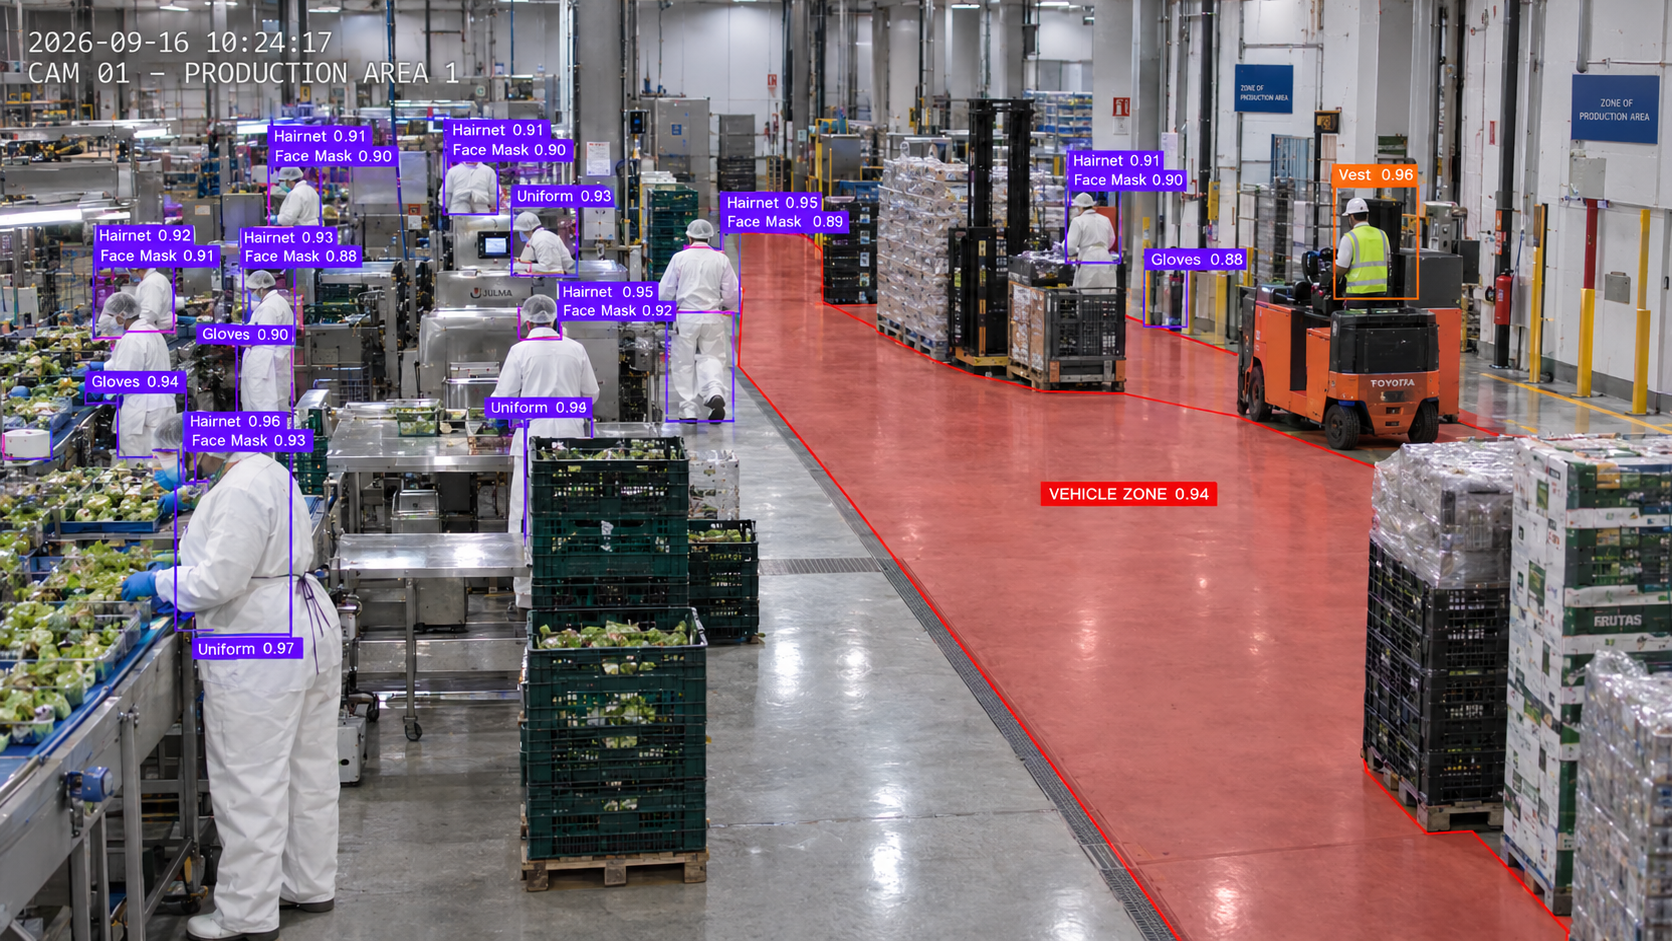
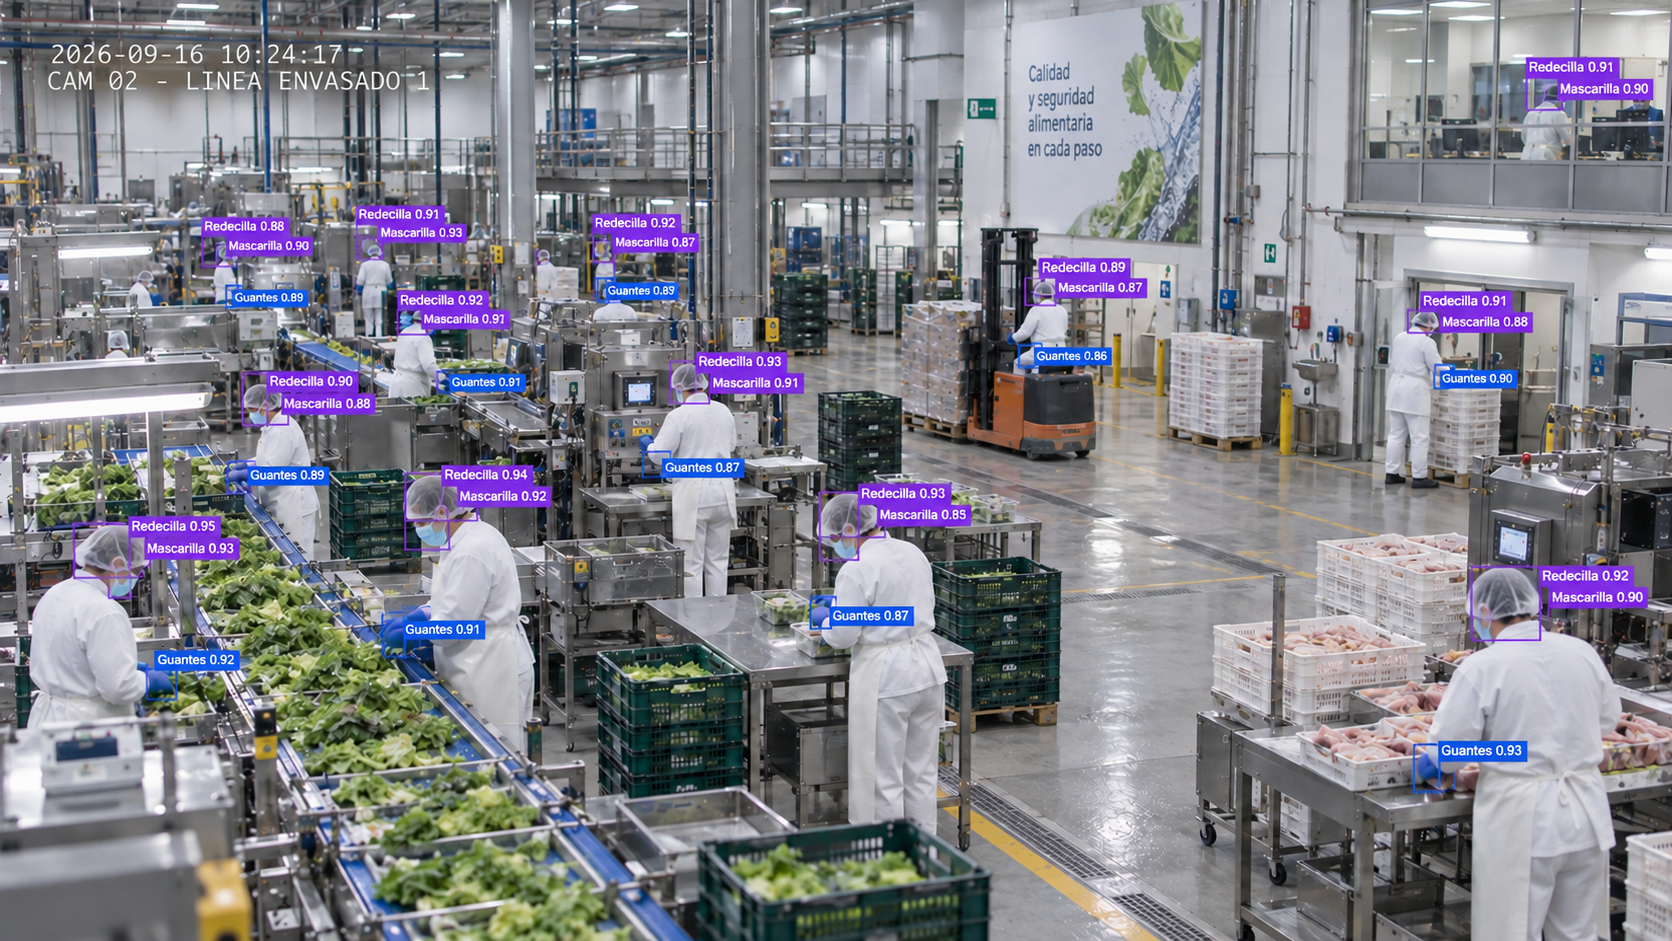
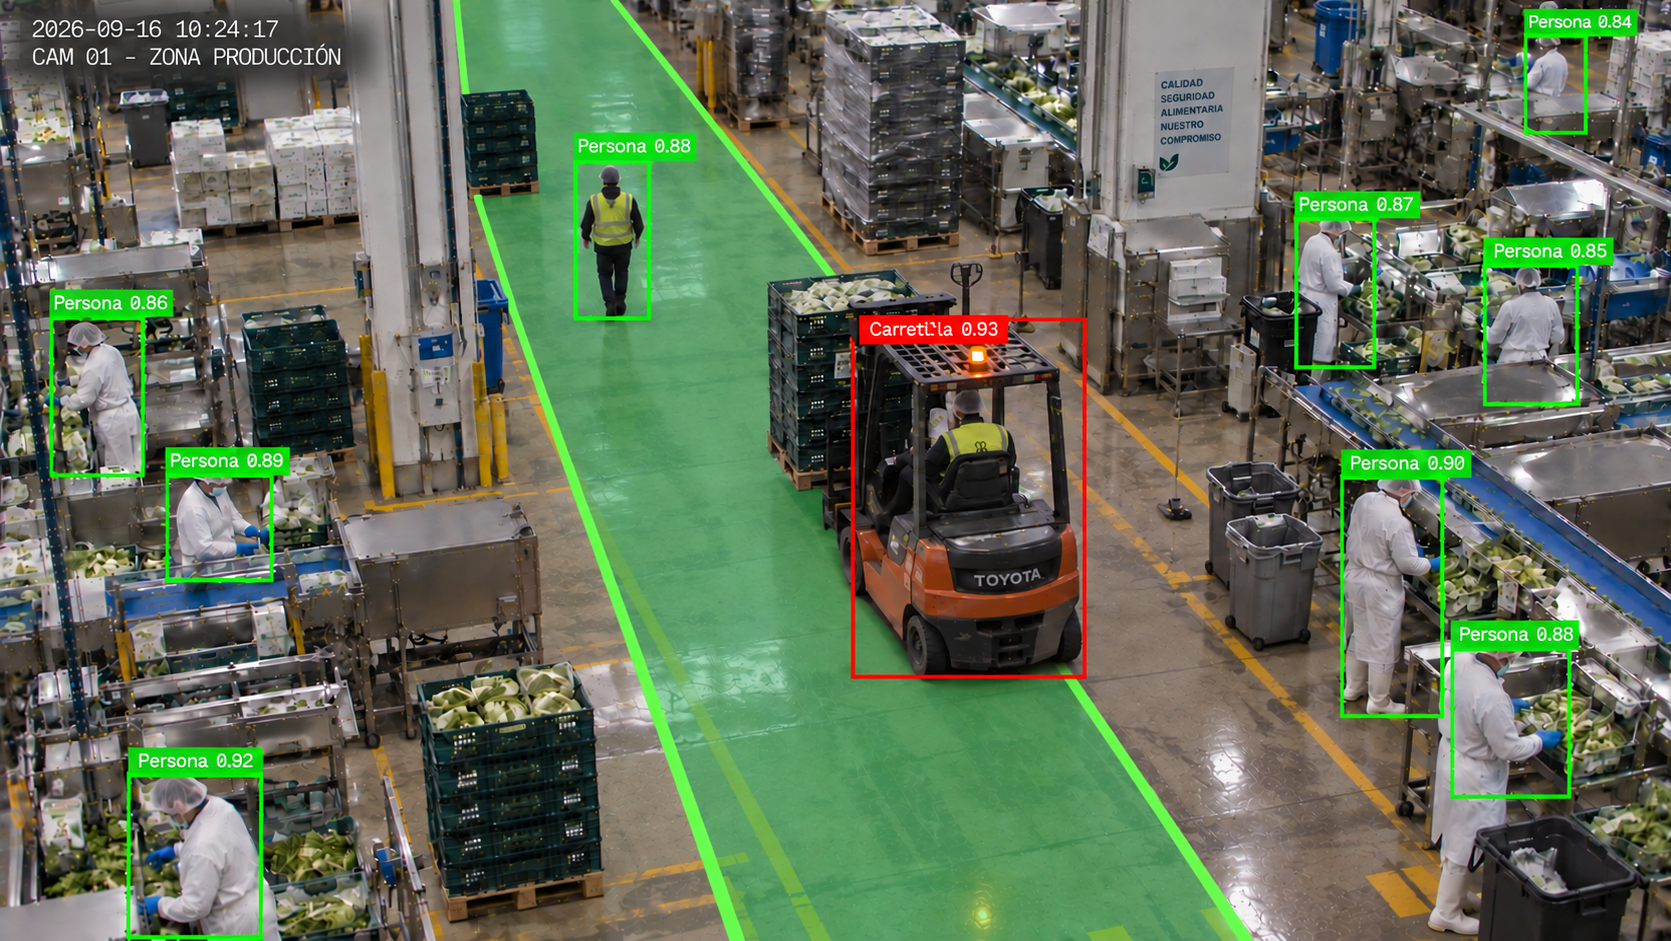
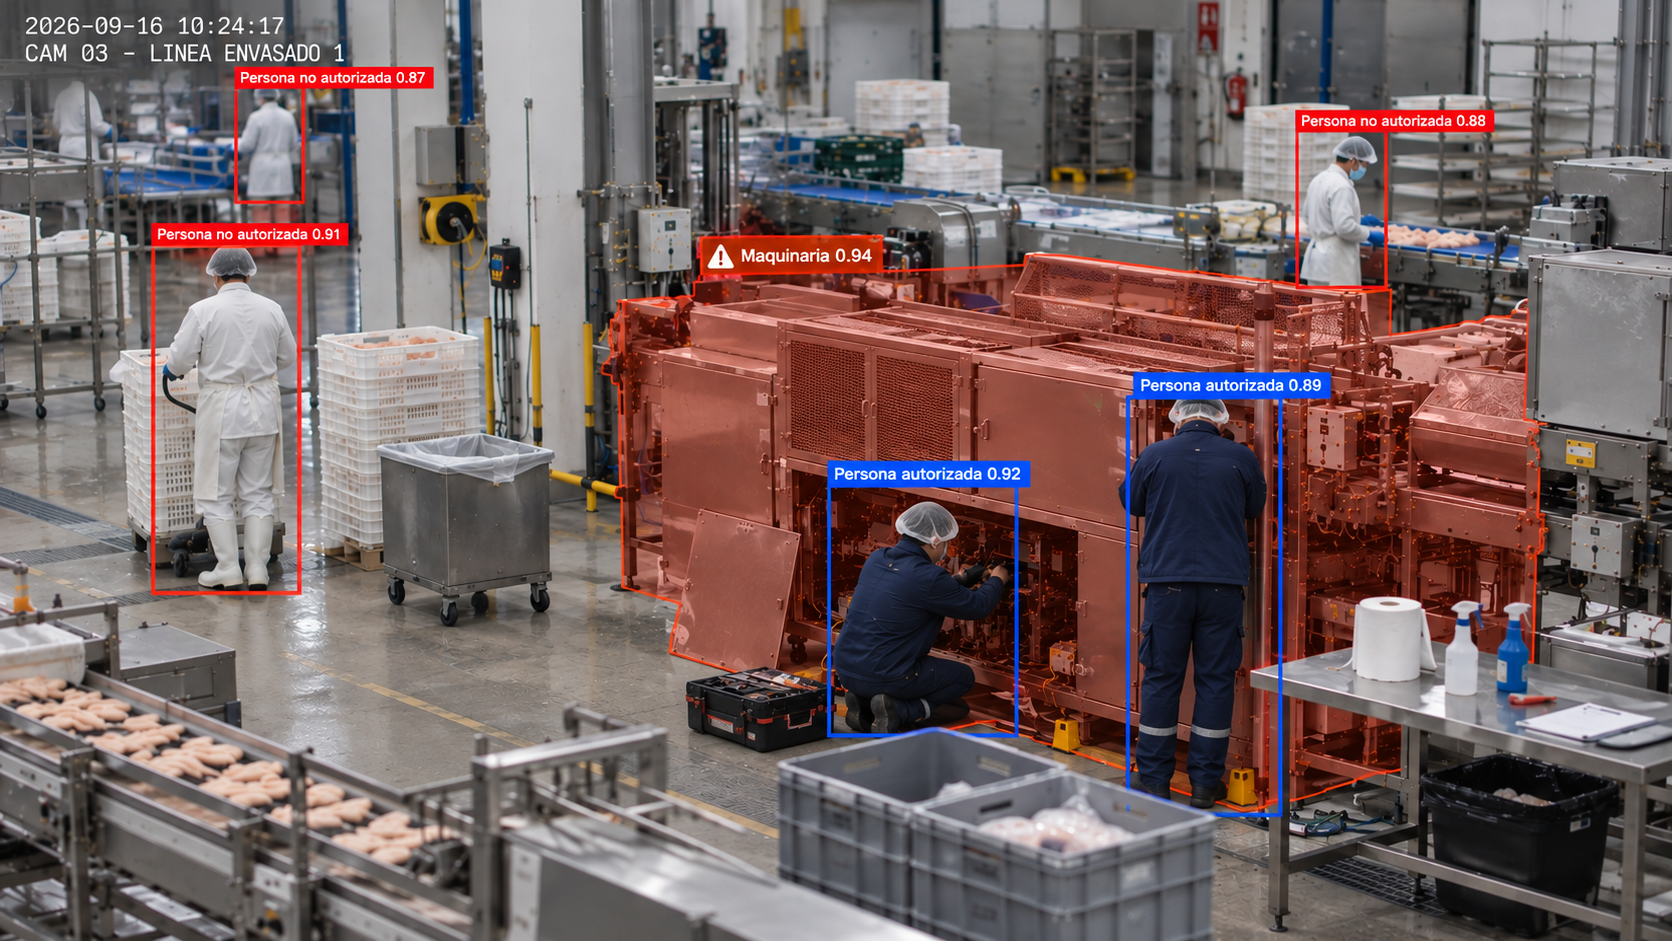
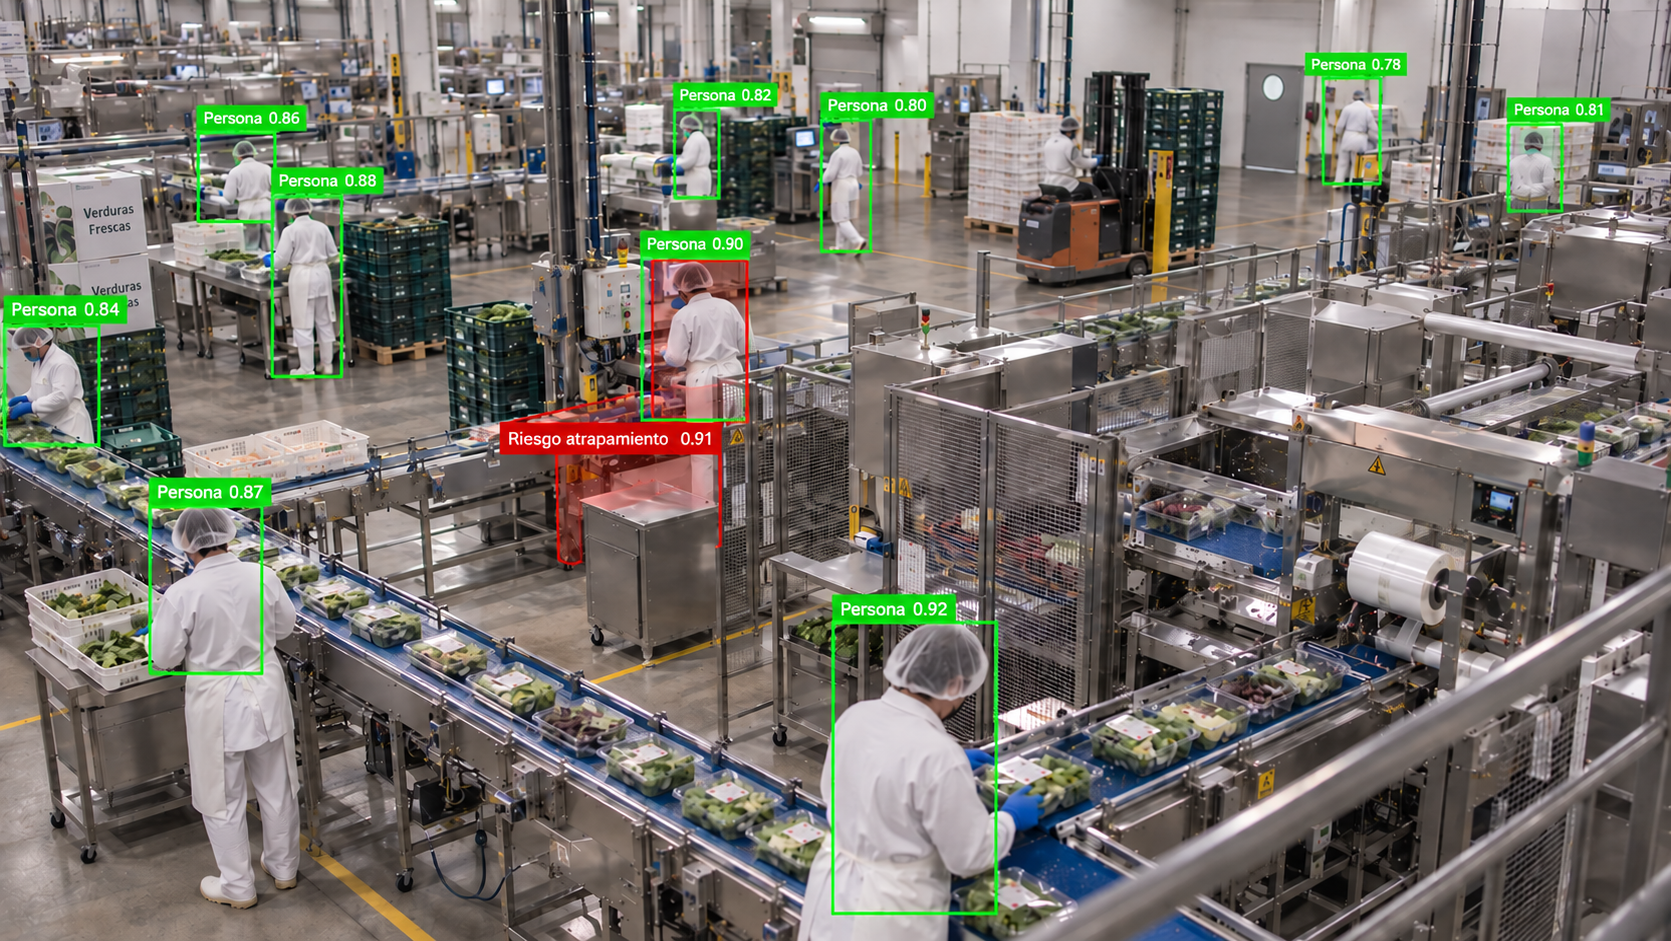
In food processing plants, production, machinery, maintenance, and foot traffic continuously coexist. Safe uses AI and computer vision to detect risk situations in real time, helping you act before an accident occurs.

Occupational Health & Safety in the food industry

Critical risks in logistics and warehousing

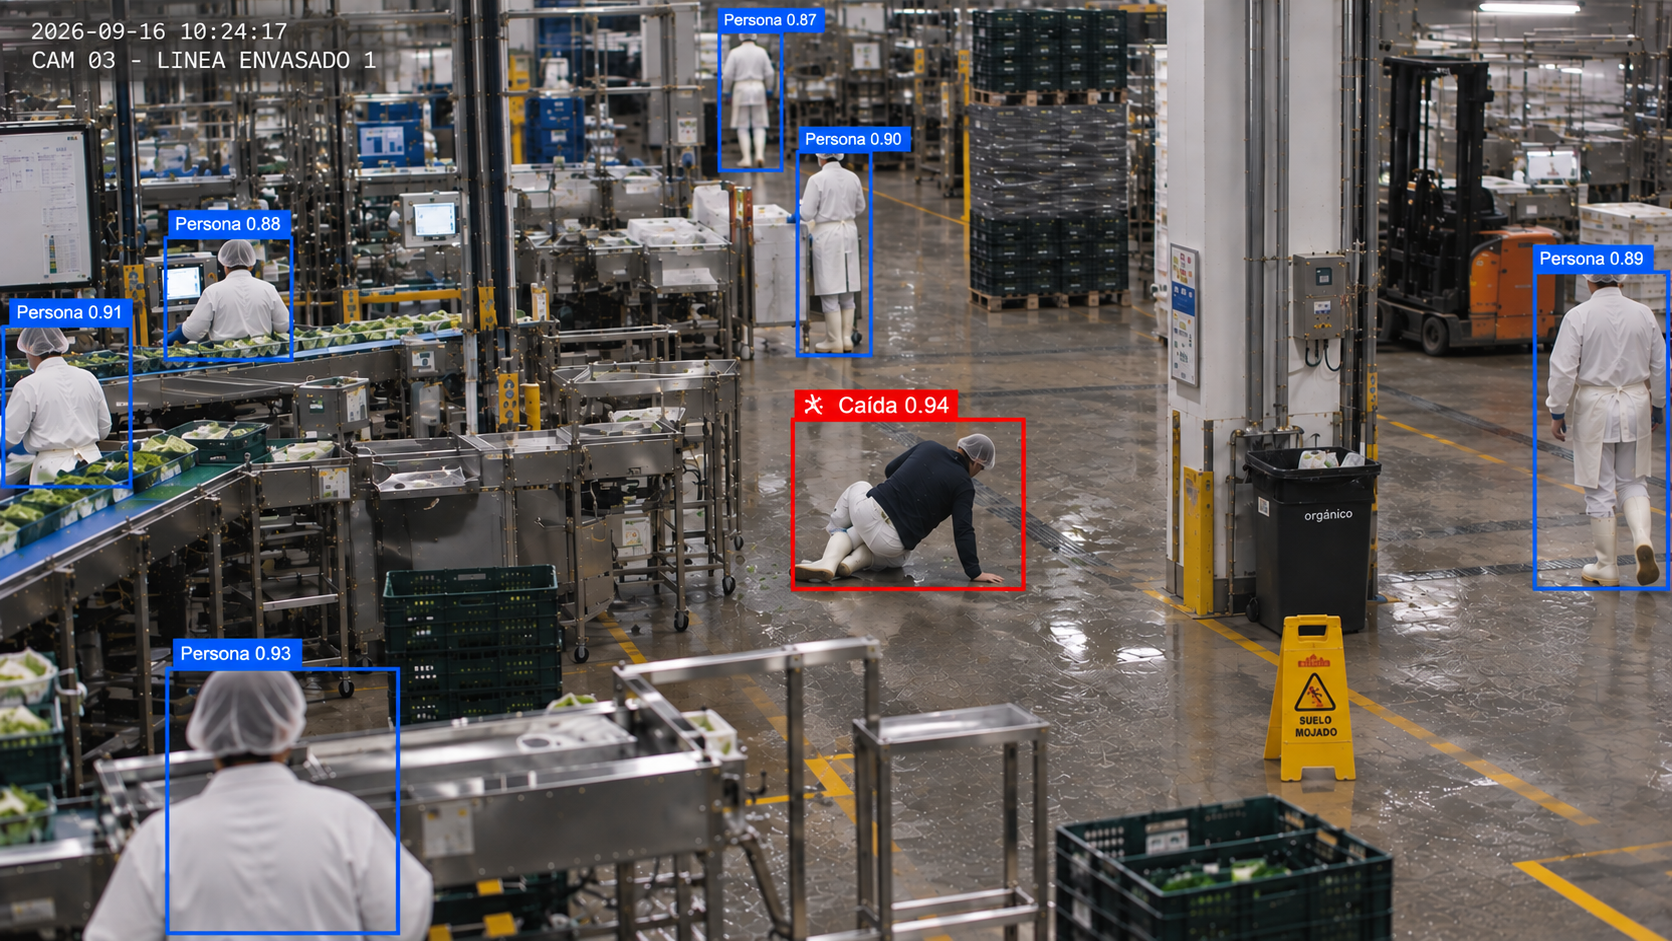
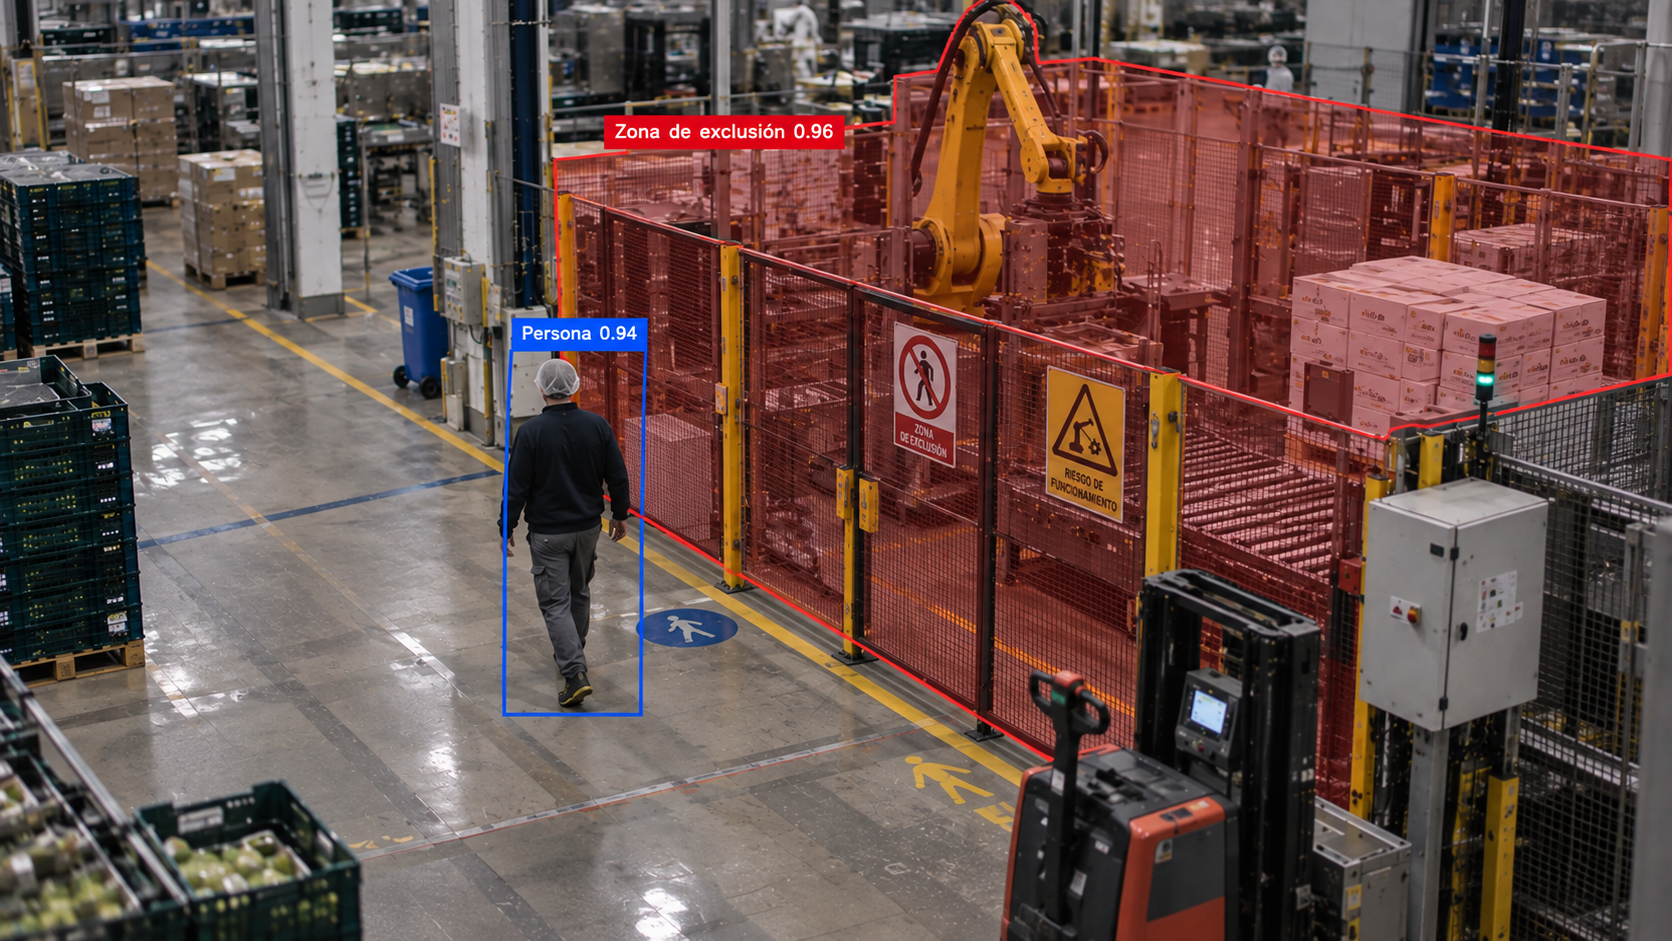
We detect and prevent the situations that cause the most incidents in industrial environments.

How Safe works

Our technology adapts to your food plant in 4 steps.

  1. 1. Detect

    Our AI cameras analyze everything happening in real time.

  2. 2. Alert

    If a risk or non-compliance is detected, an instant alert is generated.

  3. 3. Record

    All incidents are recorded with visual evidence.

  4. 4. Improve

    Reports and dashboards to make informed decisions and continuously reduce risks.
Try Safe in your own environment

Upload or drag an image of your facility and see how Safe detects risks.

Detect

Missing PPE

Or try with an example

Detection result

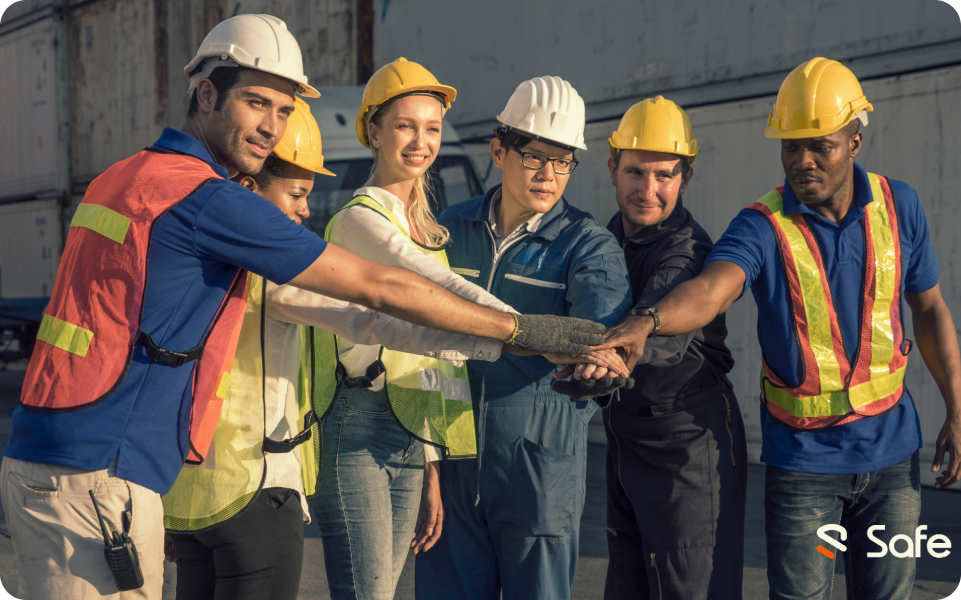
grupo de trabajadores con casco y chaleco
Try it for free with your Webcam

* Simulated result. Accuracy may vary depending on the image. Works with VLM.

icon

Using your facility's cameras

We help you comply with OHS regulations and reduce penalties.

icon

Works in minutes

Detect and prevent before accidents happen. Fewer downtime events. Greater safety.

icon

Simple, accessible to everyone

Improve productivity without compromising your team’s safety.

icon

Proactive safety for all employees

Secure data processing in full compliance with data protection regulations.

Frequently asked questions

In food processing plants, workers can be exposed to risks related to machinery, production lines, facility movement, and compliance with safety and hygiene protocols.

Computer vision enables continuous monitoring of production areas and detection of specific risk situations, helping reinforce compliance with safety measures during standard plant operations.

Safe uses computer vision to monitor the use of required personal protective equipment in work areas and identify situations where established measures are not being followed.

Want to improve safety at your plant?

Let’s talk about how Safe can help you prevent risks and protect your team.